| 1. Design and feasibility review | The supplier reviews the part drawing, material, tolerances, production volume, and intended use before recommending a process and tooling approach. | CAD files, 2D drawings, material specifications, annual demand, and quality requirements. | Confirm that drawing revisions, critical dimensions, assumptions, and proposed design changes are documented and approved. |
| 2. Tool and die design | A die is designed to cut or form sheet material. Depending on the part and production plan, tooling may be single-operation, compound, or progressive. | Die layout, tooling design, strip layout where applicable, and a defined maintenance plan. | Clarify tooling ownership, payment milestones, expected service life, maintenance responsibility, and transfer or storage terms. |
| 3. Material preparation and feeding | Sheet or coil stock is identified, inspected, and fed into the press manually or through an automated feeding system. | Common materials include low-carbon steel, stainless steel, aluminum, and copper alloys. Material grade and thickness are part-specific. | Specify grade, temper, thickness tolerance, surface condition, material certifications, and requirements for lot traceability. |
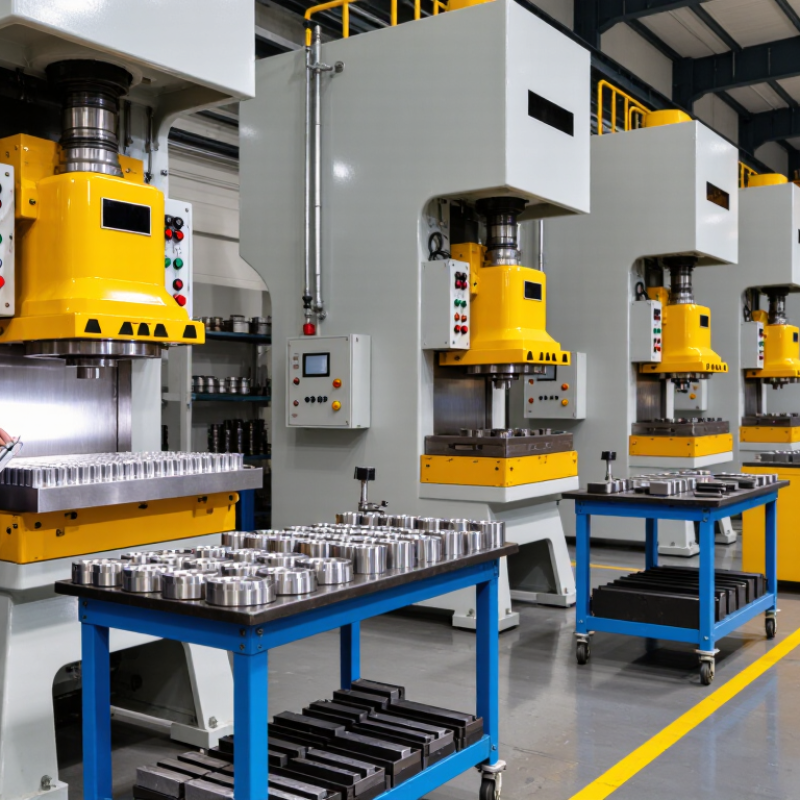
| 4. Press stamping operations | A press drives the die to cut or shape the material. Operations can include blanking, piercing, bending, forming, and drawing; a part may require more than one operation. | A press with suitable force, bed size, stroke, and feeding setup, matched to the part and tooling. | Ask how the supplier validates press capacity, process controls, setup approval, and production consistency for the specific part. |
| 5. Secondary operations | Parts may be deburred, tapped, welded, heat-treated, plated, coated, or assembled after stamping when the design requires it. | Finished or semi-finished components, with processes selected according to drawing and performance requirements. | Identify which steps are performed in-house or subcontracted, and define finish standards, inspection records, and change controls. |
| 6. Inspection and validation | The supplier checks parts against agreed requirements using suitable gauges, measuring equipment, visual checks, and documented inspection plans. | Dimensional results, material records, appearance checks, and initial sample or production validation documents as agreed. | Agree on critical-to-quality features, sampling frequency, acceptance criteria, calibration controls, and nonconformance response. |
| 7. Packaging and delivery | Parts are protected, identified, packed, and shipped according to the agreed logistics plan and destination requirements. | Packaging specification, shipment labels, delivery schedule, and export documents where applicable. | Confirm packaging protection, labeling language, shipment terms, lead-time assumptions, and procedures for shortages or transit damage. |
| Supplier comparison dimensions |
| Technical fit | Assess whether the supplier's process, equipment, tooling, and finishing capabilities match the part requirements. | Capability should be demonstrated against the buyer's actual drawings and production needs. | Request a documented feasibility review and evidence relevant to the specific application. |
| Quality systems and traceability | Review how the supplier controls materials, processes, inspections, records, and corrective actions. | Required certifications and records vary by industry, customer, and product risk. | Verify applicable certifications directly and define the records that must accompany or be retained for each lot. |
| Total landed cost | Compare the full commercial picture rather than piece price alone. | Consider tooling, material, secondary processes, packaging, freight, duties, and quality-related costs. | Request itemized quotations with clear assumptions, currency, validity period, delivery terms, and cost-change triggers. |
| Supply continuity and communication | Evaluate the supplier's planning, escalation, and communication arrangements for ongoing orders. | Capacity, lead times, business continuity arrangements, and response processes should be confirmed for the program. | Agree on forecast sharing, order confirmation, change notification, escalation contacts, and contingency expectations. |