| Material Standards and Product Classification |
| General-purpose galvanized pipe | ASTM A53/A53M | Seamless or welded carbon steel pipe for mechanical and pressure applications; Grade B is widely specified. | NPS 1/8 to NPS 26, depending on product type and manufacturer capability. | Material grade, manufacturing process, pipe type, heat number, dimensional inspection, and certificate of compliance. |
| High-temperature service pipe | ASTM A106/A106M | Seamless carbon steel pipe for elevated-temperature service; Grades A, B, and C are available. | Commonly supplied from small diameters through large nominal sizes, subject to wall-thickness limits. | Confirm that galvanizing is compatible with the intended service and that the base pipe complies with the specified A106 grade. |
| Oil, gas, and pipeline service | API 5L / ISO 3183 | Line pipe grades include PSL 1 and PSL 2 requirements; Grade B has a typical minimum yield strength of 35 ksi and tensile strength of 60 ksi. | Outside diameters and wall thicknesses are selected according to the pipeline design and applicable line-pipe specification. | PSL level, grade, impact-testing requirements, sour-service requirements, NDE scope, and full traceability. |
| European threaded and plain-end tube | EN 10255 | Non-alloy steel tubes suitable for welding and threading; S195T has a nominal minimum yield strength of 195 MPa. | Light, medium, and heavy series; commonly used for water, air, low-pressure fluids, and general installations. | Series designation, outside diameter, wall thickness, thread type, end condition, and EN 10255 inspection documents. |
| Hot-dip galvanized coating | ASTM A123/A123M or EN ISO 1461 | Coating requirements depend on the product category, steel thickness, and applicable standard; coating thickness or mass must be measured and documented. | Continuous or batch hot-dip galvanizing, depending on pipe size, production route, and order quantity. | Coating standard, average and local coating thickness, adhesion, visual condition, repair method, and test records. |
| Threaded connections | ASME B1.20.1 | NPT pipe threads are commonly used in North American installations; other regional thread profiles may apply. | Threaded ends are normally offered on smaller nominal sizes; larger sizes are often supplied plain-end or bevel-end. | Thread standard, taper, gauge inspection, thread protector use, coupling supply, and compatibility with fittings. |
| Dimensional tolerances | Product standard and ASME B36.10M reference dimensions | Outside diameter, wall thickness, length, ovality, straightness, and mass tolerances must follow the selected product standard. | Random lengths are often approximately 4.8–6.7 m; fixed lengths can be produced to order within mill and cutting limits. | Permitted tolerance values, actual measured dimensions, length tolerance, end squareness, and packing method. |
| Common Round Pipe Dimensions |
| NPS 1/2 / DN 15 | ASME B36.10M nominal dimensions | Outside diameter: 0.840 in / 21.3 mm; Schedule 40 wall: 0.109 in / 2.77 mm. | Typical uses include small water, air, drainage, and instrument-support lines. | Confirm actual outside diameter, wall thickness, threading allowance, and internal zinc buildup. |
| NPS 1 / DN 25 | ASME B36.10M nominal dimensions | Outside diameter: 1.315 in / 33.4 mm; Schedule 40 wall: 0.133 in / 3.38 mm. | Common for building services, compressed air, water distribution, and low-pressure systems. | Confirm schedule, pressure-design basis, end type, and fitting compatibility. |
| NPS 2 / DN 50 | ASME B36.10M nominal dimensions | Outside diameter: 2.375 in / 60.3 mm; Schedule 40 wall: 0.154 in / 3.91 mm. | Frequently used in fire-water, utility, agricultural, and general mechanical installations. | Verify dimensional tolerance, coating uniformity, coupling or flange connection requirements, and hydrostatic test documentation. |
| NPS 4 / DN 100 | ASME B36.10M nominal dimensions | Outside diameter: 4.500 in / 114.3 mm; Schedule 40 wall: 0.237 in / 6.02 mm. | Suitable for larger water, utility, structural, and industrial piping systems when design conditions permit. | Check lifting, bundling, end protection, straightness, internal cleanliness, and coating repair procedures. |
| NPS 6 / DN 150 | ASME B36.10M nominal dimensions | Outside diameter: 6.625 in / 168.3 mm; Schedule 40 wall: 0.280 in / 7.11 mm. | Common in industrial utilities, water networks, sprinkler mains, and large mechanical systems. | Confirm flange dimensions, bevel geometry, wall-thickness measurement method, and transport protection. |
| NPS 8 / DN 200 | ASME B36.10M nominal dimensions | Outside diameter: 8.625 in / 219.1 mm; Schedule 40 wall: 0.322 in / 8.18 mm. | Used for high-flow utility, process, cooling-water, and fire-protection applications. | Verify dimensional control, weld quality where applicable, coating continuity, handling equipment, and site joining method. |
| NPS 12 / DN 300 | ASME B36.10M nominal dimensions | Outside diameter: 12.750 in / 323.9 mm; Schedule 40 wall: 0.375 in / 9.53 mm. | Used in large-diameter water, utility, industrial, and infrastructure systems subject to engineering design. | Confirm production route, maximum available length, weld inspection, coating thickness mapping, and loading plan. |
| Performance and Quality Requirements |
| Mechanical strength | Specified material standard | For ASTM A53 Grade B, typical minimum values are 35 ksi / 240 MPa yield strength and 60 ksi / 415 MPa tensile strength. | Values vary by grade, standard, product form, and test direction. | Review mill test certificates, heat number traceability, tensile results, yield results, and elongation results. |
| Pressure capability | Engineering design code and product standard | Pressure rating is not determined by nominal size alone; it depends on material strength, wall thickness, temperature, weld factor, corrosion allowance, and design code. | Use the purchaser’s design pressure, temperature, fluid, and safety-factor requirements. | Request a design calculation or rating basis rather than relying only on a generic working-pressure claim. |
| Hydrostatic or nondestructive testing | ASTM, API, EN, or project specification | Testing may include hydrostatic testing, ultrasonic testing, electromagnetic testing, radiography, or visual inspection, depending on the standard. | Test scope should be stated in the purchase order and inspection plan. | Confirm test pressure or test method, duration, acceptance criteria, calibration records, and retest policy. |
| Coating uniformity | ASTM A123/A123M or EN ISO 1461 | Coating should be continuous and substantially free from bare spots, excessive runs, blisters, flaking, and harmful inclusions. | Minor surface variations may occur after hot-dip galvanizing, but functional defects require evaluation and repair. | Check magnetic thickness readings, sampling plan, visual inspection records, and approved zinc-rich repair materials. |
| Corrosion-service suitability | Project corrosion-control specification | Galvanized steel performs well in many atmospheric and water-service environments, but performance depends on pH, chlorides, temperature, flow, and exposure. | Do not assume suitability for continuously immersed, highly acidic, highly alkaline, or high-temperature service without technical review. | Request a corrosion assessment, service-temperature limit, water chemistry review, and compatibility confirmation. |
| Welded-pipe weld quality | Applicable product standard and purchase specification | Welded pipe should have a controlled longitudinal or spiral weld process with appropriate inspection and dimensional control. | Inspection level varies by ASTM, API, EN, or project requirements. | Verify welding procedure controls, NDE percentage, weld repair policy, weld-location records, and operator qualifications. |
| End preparation | Product standard and purchaser specification | Available ends include plain end, beveled end, threaded end, and grooved end; bevel geometry must match the joining procedure. | Plain and beveled ends are common for welded or flanged systems; threaded ends are common for smaller sizes. | Confirm bevel angle, root face, thread protection, groove dimensions, burr removal, and end-cap requirements. |
| Traceability and documentation | EN 10204 inspection-document system or equivalent project requirement | Typical documentation includes material certificate, coating report, dimensional report, test report, packing list, and certificate of conformity. | 3.1 inspection certificates are commonly requested for critical industrial applications. | Ensure heat numbers remain legible through galvanizing, bundling, delivery, and final installation. |
| Supplier capability benchmark | Purchaser qualification procedure | Preferred suppliers should demonstrate standard compliance, stable production capacity, quality-control systems, export packing, and repeatable dimensional performance. | Evaluate sample approval, production lead time, minimum order quantity, customization, and inspection support. | Compare verified test records, audit results, sample quality, delivery history, technical response time, and after-sales handling. |
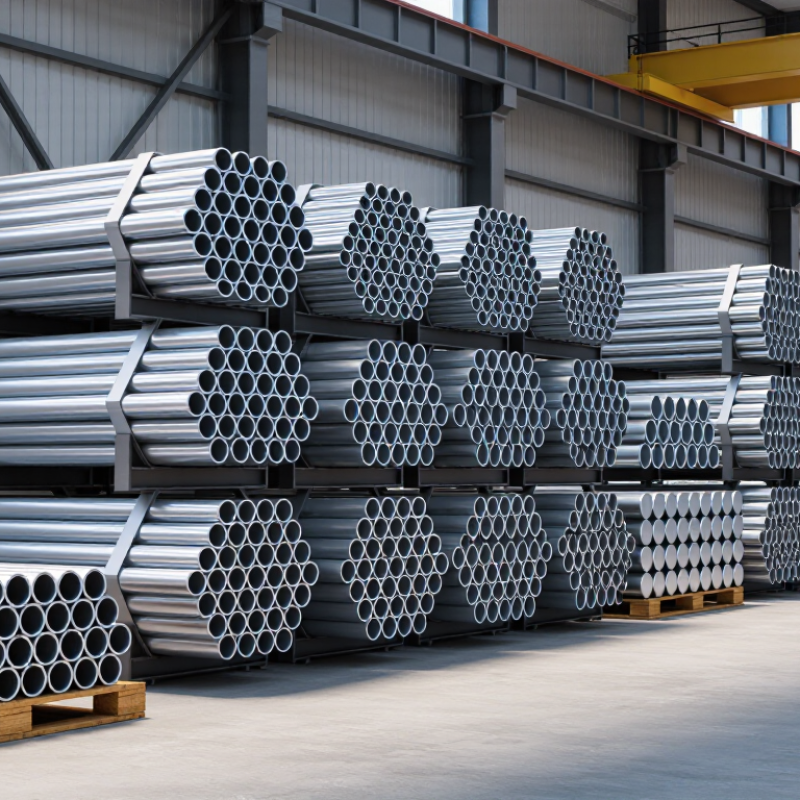
| Packaging and transport protection | Project logistics specification | Pipe should be bundled securely with separators or protective materials that minimize coating damage, deformation, contamination, and water entrapment. | Suitable for truck, container, break-bulk, or long-distance multimodal transport. | Confirm bundle weight, lifting points, end caps, moisture protection, marking, container loading plan, and storage instructions. |