| Metal Hazard Scope | Metal fragments may enter through damaged screens, mixers, conveyors, cutters, bearings, fasteners, maintenance work or packaging equipment. | Include ferrous, non-ferrous and stainless-steel contamination in the hazard analysis and validation plan. | Different metal types have different electromagnetic responses. A detector should be assessed against the materials that could realistically occur on the biscuit line. | High |
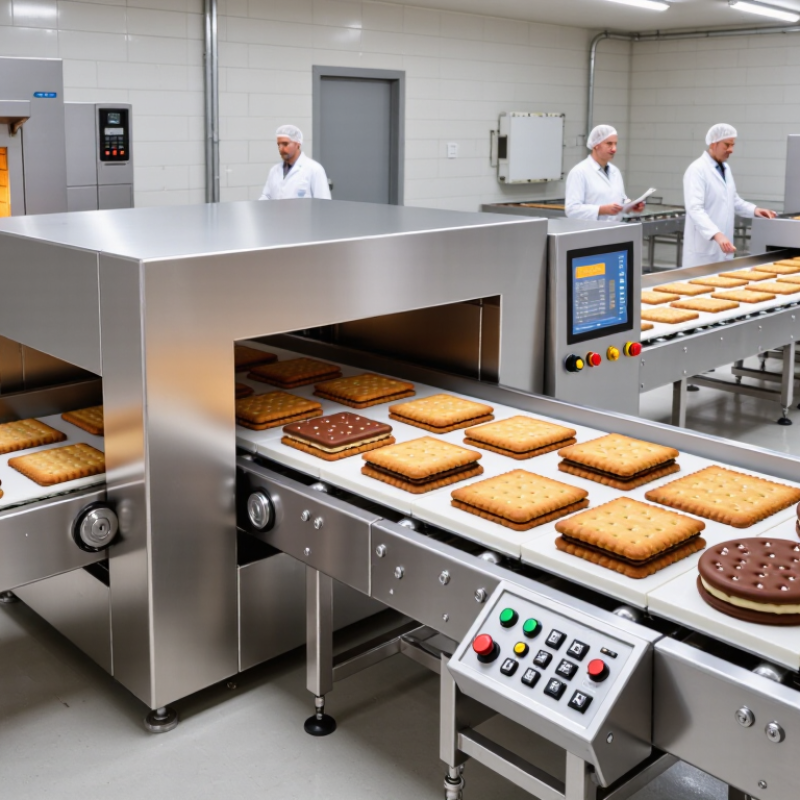
| Product Form | Biscuits may be inspected as loose products, multipacks, cartons or cases, depending on the process layout. | Select the detector configuration for the actual inspection point, product orientation, conveyor width, aperture size and packaging format. | Detection performance is affected by aperture size, product presentation, line speed and whether the product is inspected individually or in a package. | High |
| Product Effect | Dry biscuits generally have less product effect than wet or highly conductive foods, but recipes containing salt, minerals, fillings, inclusions or moisture can change detector stability. | Validate the detector using representative products from the most challenging recipe, moisture condition and package format. | Detector sensitivity cannot be selected reliably from a generic catalogue value alone. The finished product and operating environment must be tested. | High |
| Critical Control Point Decision | Metal detection may be identified as a CCP when it is the final or essential control that prevents contaminated product from reaching the consumer. | Use the HACCP team’s hazard analysis and decision process to determine whether the detector is a CCP or another control measure. | Codex CXC 1-1969 requires controls to be appropriate to the identified hazard; it does not automatically classify every detector as a CCP. | High |
| Detection Performance | Detection capability depends on the detector design, aperture, product effect, line speed, vibration, electrical interference and test-piece position. | Establish site-specific validated limits for ferrous, non-ferrous and stainless-steel test pieces. Do not treat universal test-piece sizes as automatically applicable. | Codex sets food-hygiene and HACCP principles rather than one mandatory sensitivity level. The limit must be justified by risk assessment and validation evidence. | High |
| Automatic Reject System | A contaminated product must be reliably removed without allowing rejected items to return to the acceptable product stream. | Use a fail-safe reject arrangement suitable for the line, with controlled collection, reject confirmation where appropriate, and protection against bypass. | A detector alarm without dependable product segregation does not provide effective hazard control. | High |
| Reject Security | Rejected biscuits may be accidentally reintroduced, mixed with good product or discarded without investigation. | Control the reject container, restrict access, identify rejected product, and define disposition by an authorized person. | Product segregation and corrective action are necessary to prevent potentially unsafe product from being released. | High |
| Routine Monitoring | The detector can drift or become ineffective because of setup changes, faults, vibration, contamination, incorrect settings or environmental interference. | Define documented checks at start-up, after product or setting changes, after interruptions, and at a risk-based frequency during production. | Monitoring demonstrates that the control remains within its validated operating conditions. | High |
| Test-Piece Procedure | Test pieces must challenge the complete inspection and rejection system, not only the detector sensor. | Use identifiable, calibrated or verified test pieces; pass them through representative product at defined positions and record the result. | Testing should demonstrate detection, alarm, rejection and product segregation under normal operating conditions. | High |
| Corrective Action | A failed test, unexplained alarm or reject-system fault may leave product made since the last satisfactory check in question. | Stop or control the line, place affected product on hold, investigate the cause, restore verified performance, re-screen or disposition product, and document the action. | Corrective action prevents the release of product manufactured while the CCP or control measure may not have been effective. | High |
| Validation | The selected detector and operating limits must be capable of controlling the identified metal hazard before routine use. | Validate with actual biscuit products, packaging, line speed, aperture, environmental conditions and worst-case operating scenarios. | Validation provides objective evidence that the control measure can work as intended; it is different from routine monitoring. | High |
| Verification | Even a validated system may fail if procedures are not followed or equipment performance deteriorates. | Review monitoring and corrective-action records, audit procedures, assess trends, and periodically confirm detector performance through an independent or formally planned verification activity. | Codex HACCP principles require verification that the HACCP system is working effectively. | Medium |
| Calibration and Maintenance | Sensor drift, damaged belts, poor alignment, loose components and unsuitable repairs can compromise detection or rejection. | Maintain a preventive-maintenance and calibration or performance-check schedule based on manufacturer instructions, site history and risk. | Equipment condition is part of prerequisite programmes and supports consistent operation of the hazard control. | Medium |
| Hygienic Design | Biscuits and crumbs can accumulate around equipment, while difficult-to-clean areas can create sanitation and pest risks. | Choose food-contact-compatible materials and a cleanable, accessible design that suits the plant’s dry-cleaning or wet-cleaning programme. | Metal detection controls physical hazards but does not replace good hygiene, sanitation and allergen controls. | Medium |
| Environmental Suitability | Electrical noise, temperature changes, vibration, dust, water ingress and nearby metal structures may affect performance. | Install and operate the equipment within its specified environmental conditions and assess interference during validation. | Stable environmental conditions reduce nuisance alarms and the risk of undetected performance loss. | Medium |
| Traceability and Records | Investigations require evidence of which product, line, time period and detector status were involved. | Record product and lot identification, detector settings, test results, alarms, rejects, holds, corrective actions, release decisions and responsible personnel. | Complete records support HACCP verification, product disposition and regulatory or customer audits. | High |
| Selection Conclusion | There is no single universally best metal detector for every biscuit facility. | The best choice is the system that achieves validated performance on the actual biscuit product and packaging, provides dependable automatic rejection, supports hygienic operation, and fits the site’s HACCP procedures. | Selection should be based on documented risk, validation evidence, operating reliability and maintainability rather than brand reputation alone. | Decision Rule |