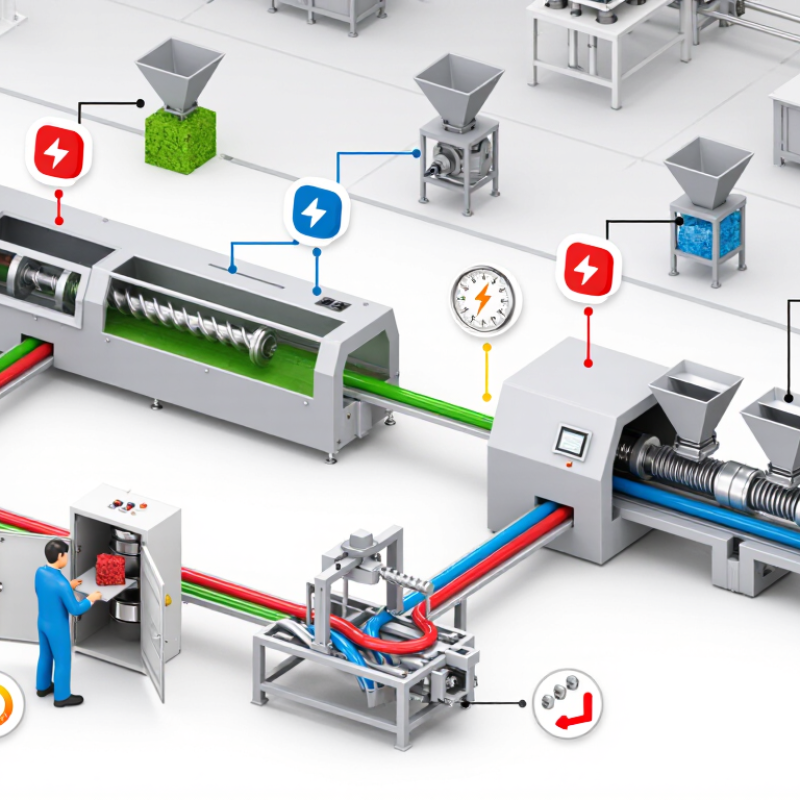
| Single-screw extruder | One rotating screw conveys, melts, and pressurizes material through a heated barrel. | Polyethylene (PE), polypropylene (PP), polystyrene (PS), and many PVC formulations. | Pipe, profiles, film, sheet, pelletizing, and general-purpose extrusion. | About 20–1,000 kg/h, depending on screw diameter, material, and product. | Continuous production of a consistent, well-prepared feedstock. | Usually economical and straightforward, but less effective than twin-screw designs for intensive mixing or highly variable feed. |
| Co-rotating twin-screw extruder | Two intermeshing screws rotate in the same direction, supporting strong conveying and distributive and dispersive mixing. | Engineering plastics, filled or reinforced polymers, color concentrates, and polymer blends. | Compounding, masterbatch production, devolatilization, and reactive processing. | About 10–1,500 kg/h; smaller machines are often used for specialty formulations. | Formulations that need controlled mixing, additive dispersion, or frequent recipe changes. | Offers process flexibility, but typically requires a higher equipment investment and more process expertise than a basic single-screw line. |
| Counter-rotating twin-screw extruder | Two screws rotate in opposite directions; intermeshing designs provide positive conveying and relatively controlled melt handling. | Rigid and flexible PVC compounds, including heat-sensitive formulations. | PVC pipe, window profiles, siding, and other PVC profiles. | About 30–1,000 kg/h, depending on machine size, formulation, and product. | PVC processing where steady conveying and careful temperature management are important. | Screw and barrel configuration is usually tailored to the PVC formulation and intended product. |
| Ram (plunger) extruder | A reciprocating ram pushes softened or prepared material through a die rather than using a continuously rotating screw. | Selected high-viscosity, heat-sensitive, or difficult-to-convey materials; use is specialized. | Specialty profiles, laboratory work, and processes where screw shear or continuous screw conveying is unsuitable. | Often about 5–100 kg/h; highly dependent on the material and operating cycle. | Low-volume or specialized processing where material behavior favors ram-driven flow. | Generally less suited to high-throughput continuous production than screw extruders. |