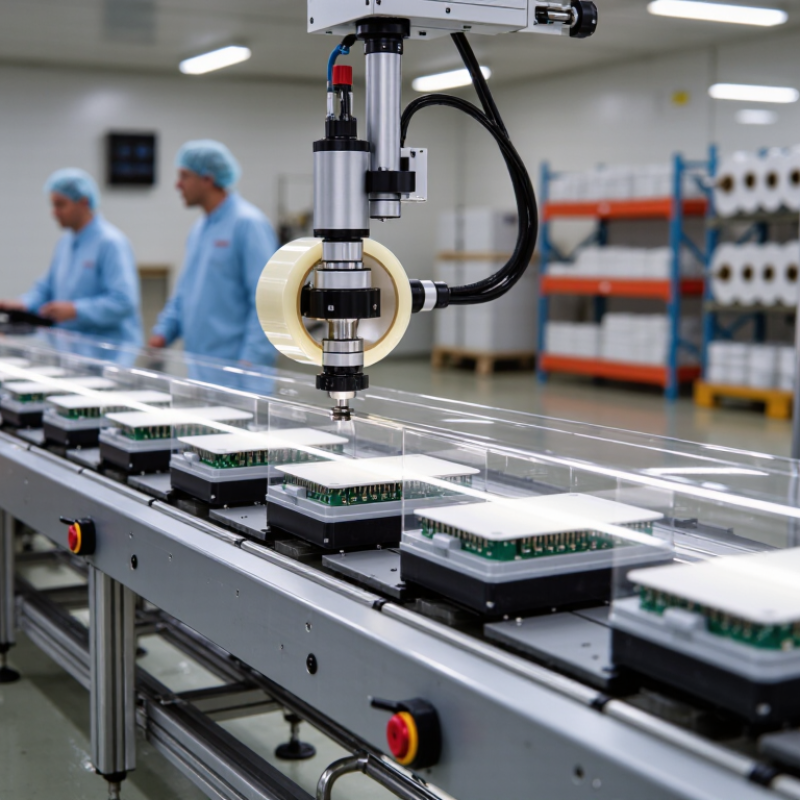
Choosing the best Heat Sealing Cover Tape in 2026 requires more than comparing prices or browsing technical datasheets. The right tape must match the carrier material, component geometry, sealing temperature, peel strength, and storage conditions. A tape that performs well on a clean laboratory bench may behave differently beside a fast production line. Small changes matter. Dust, humidity, pressure, and dwell time can alter the result.
Dr. Jay Singh, a recognized packaging engineering researcher, offers a useful principle: “A seal is only reliable when material, machine, and environment work together.” This view keeps the selection process practical. Buyers should examine seal consistency, peel behavior, residue, transparency, and compatibility with automated equipment. They should also request test samples and record results under real operating conditions. Marketing claims are not enough.
This guide compares the main factors behind a dependable Heat Sealing Cover Tape choice for 2026. It considers recyclable packaging goals, high-speed sealing, sensitive components, and changing supply requirements. Some recommendations may still need adjustment. No universal tape exists. A material that works perfectly for small electronic parts may fail on a wider carrier or different sealing tool. That is an uncomfortable detail, but ignoring it creates expensive rework. Careful testing remains the most trustworthy path. Expect surprises. Perfect certainty is rare.
How to Choose the Best Heat Sealing Cover Tape in 2026?
Selecting cover tape starts with the pocket, not the sealing machine. EIA-481 defines carrier-tape dimensions, pocket tolerances, and indexing requirements for automated component handling. Measure the pocket length, width, and depth before choosing tape.
A 12 mm carrier may need 12 mm cover tape, but the actual sealing window can vary by equipment. Common options include 8, 12, 16, and 24 mm widths.
SEMI’s 2024 World Fab Forecast reported continued expansion in global semiconductor manufacturing capacity through 2025. More capacity means more packaged components moving through high-speed assembly lines. That increases the need for stable peel force, clean release, and reliable protection against moisture and dust.
Industry packaging reports also identify thinner devices and denser pocket layouts as continuing design trends. Therefore, test the tape with the real pocket geometry, not a similar sample.
Check seal temperature, dwell time, peel angle, and line speed together. A tape that opens neatly at 0.3 N may fail after storage or transport vibration. This is often missed.
Record peel-force results across several reels, because one sample cannot represent production variation. I would also inspect exposed component surfaces after peeling. Residue, lifted parts, or torn sealing layers indicate a mismatch.
EIA-481 gives the framework, but the final choice still depends on material surface, pocket depth, and machine behavior. Perfect specifications can still produce imperfect results.