| Press Brake |
A punch and die bend sheet or plate along a straight axis. CNC controls can coordinate the back gauge and bending sequence. |
Flat sheet and plate, formed into channels, brackets, panels, and enclosures. |
Versatile for different part shapes and short production runs; tooling can be changed for different bends. |
Primarily makes straight-line bends; complex parts may require multiple setups and careful bend sequencing. |
Job shops and manufacturers producing varied bent-sheet components. |
| Mechanical Stamping Press |
A motor-driven flywheel and crank or eccentric mechanism move a ram through a repeated stroke to shear or form sheet metal. |
Sheet-metal parts made with dies, including pierced, blanked, and shallow-formed components. |
Fast, repeatable strokes make it suitable for high-volume production with dedicated tooling. |
Tooling can be costly; setup changes and stroke characteristics may limit flexibility for some operations. |
Large production runs of consistent parts using established dies. |
| Hydraulic Press |
Hydraulic cylinders apply force to a ram, allowing pressure to be maintained during a forming operation. |
Sheet, plate, and other workpieces used in forming, deep drawing, or pressing operations, depending on tooling. |
Force and ram motion can be controlled across the stroke; useful for operations that need sustained pressure. |
Typically has a slower operating cycle than a high-speed mechanical press; performance depends on press design and tooling. |
Forming tasks that need controlled force, flexible settings, or longer dwell time. |
| Roll Forming Machine |
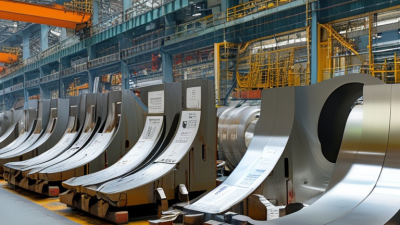
A strip or coil passes through successive roller stands, with each set gradually forming the metal profile. |
Long, continuous profiles such as channels, rails, trim, and framing sections. |
Efficient for long parts with a consistent cross-section; suitable for continuous production. |
Profile changes usually require roller tooling; it is not intended for producing arbitrary shapes along the part length. |
High-volume production of long metal profiles with a uniform cross-section. |
| Forging Press |
Compressive force from a press deforms a heated or cold metal billet in open or closed dies. |
Solid metal billets formed into components such as shafts, gears, and structural parts. |
Can produce dense, strong components; press action allows controlled deformation in the die. |
Requires appropriate dies and process planning; heating, handling, and finishing needs depend on the material and process. |
Production of solid components where forged shape and material properties are important. |
| Metal Spinning Lathe |
A rotating blank is pressed against a form or mandrel by a roller or tool to create an axisymmetric shape. |
Round, hollow parts such as cones, domes, reflectors, and cylindrical components. |
Can make seamless, rotationally symmetrical parts; tooling may be simpler than dedicated multi-part forming dies. |
Limited to rotationally symmetrical shapes; results depend on material, geometry, and operator or control setup. |
Small to medium runs of round, hollow metal parts. |